Energy Storage Cabinet Factory: A Behind-the-Scenes Look at Modern Production
2026-10-18
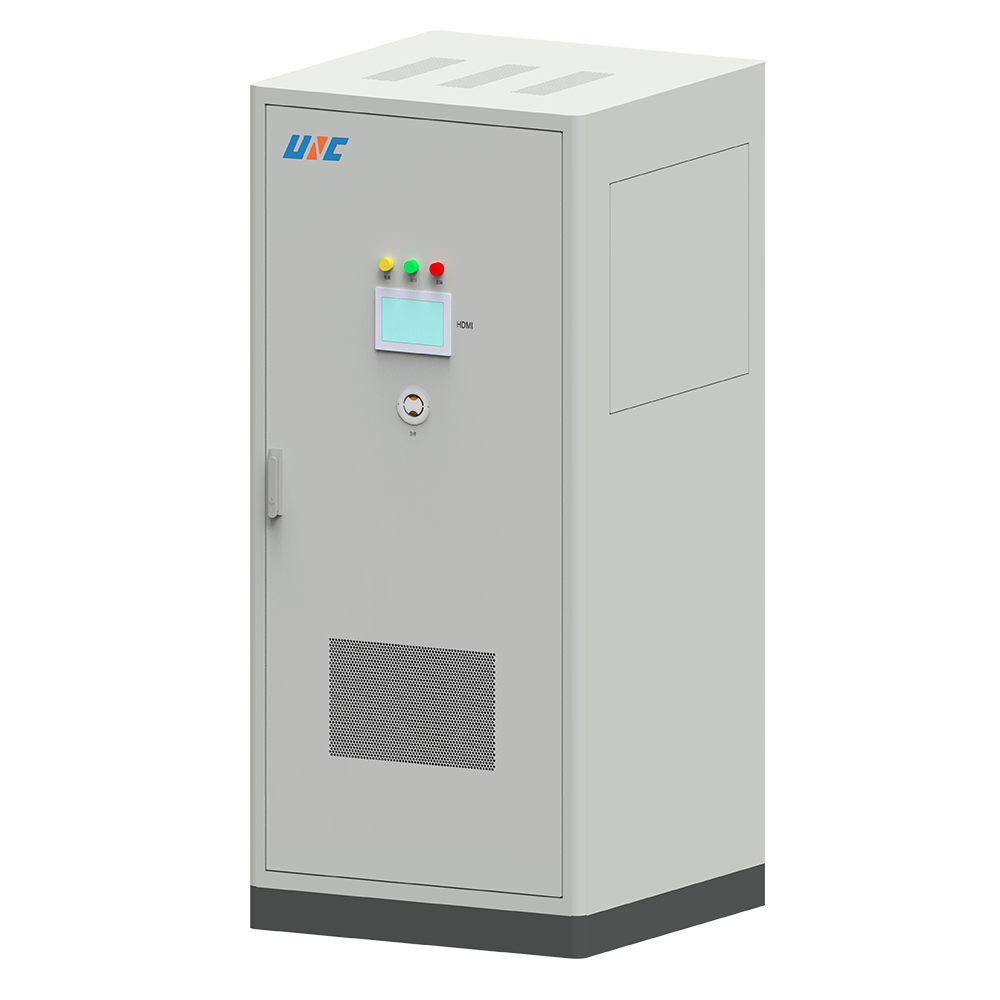
Most people never see what happens before an energy storage cabinet is bolted to a warehouse wall or tucked beside a solar array. At UNC’s factory, that hidden journey is a tightly choreographed mix of robotics, human expertise, and relentless testing. From laser-cut steel to the final firmware upload, every step decides whether the unit will survive decades of charge cycles or fail in year two. This behind-the-scenes look walks the production floor where cabinets aren’t just assembled—they’re engineered to outlast expectations.
Sheet Metal In, Smart Cabinets Out: A Floor Walk
Walking the line where raw sheet metal enters and finished smart cabinets roll out feels less like a tour and more like watching a personality shift. Coils get unspooled, laser-cut, bent, and welded into shells that still smell of ozone and hot steel. Then the second half of the floor takes over: sensors are tucked into frames, touch panels are wired, firmware is loaded, and each cabinet is tested as a connected device rather than just a box.
The quiet part isn't the machinery, it's the handoffs. Between stamping and assembly, bins carry not just parts but routing data. A cabinet destined for a hospital pharmacy gets different validation steps than one headed to a telecom hut. The floor doesn't treat them as identical units; it reads their build sheets and adjusts torque settings, firmware versions, and even final inspection checklists without a line stoppage.
By the time a cabinet reaches the dock, it already knows its own serial number, has logged its test results, and can report which technician signed off on the door alignment. That shift from inert sheet metal to a network-aware enclosure is the real story of the walk, and it happens in the same physical space where a stack of steel sat that morning.
Robotic Welding and Laser Cutting: Precision Without Pause
In a single shift, a six-axis robot can lay down hundreds of identical weld beads while a laser cutter slices through 12-gauge steel at three meters per minute—both holding tolerances tighter than a human hand could ever manage. The real advantage isn't speed alone; it's the absence of drift. Once the parameters are dialed in, the thousandth part comes out exactly like the first, with no coffee breaks, no fatigue, no subtle variation in torch angle.
Laser cutting complements the welding cell by handling contours that would require multiple fixturing steps on a CNC punch or plasma table. The beam doesn't wear down, so kerf width stays consistent from morning to night. That consistency feeds back into the welding side: parts fit better, gaps stay predictable, and the robot doesn't have to compensate for sloppy upstream cuts.
Where this combination really earns its keep is in high-mix, low-volume work. Changing from one part number to another used to mean an hour of manual reprogramming and test cuts. Now it's a file upload and a quick dry run. You still need people, but they're inspecting, tuning, and problem-solving instead of breathing fumes over a hot puddle.
The Battery Tray Tolerances Most Buyers Never See
Most buyers check the overall width and bolt-hole spread on a battery tray, call it good, and move on. What they miss are the invisible tolerances that decide whether a tray actually survives five years under a hood. A stamped tray can carry a ±1.5 mm variance on the side walls alone, and when you stack that with the ±0.8 mm from the weld fixture and another half-millimeter from the powder coat, the “perfect” fit starts looking like a gamble. Those numbers rarely show up on a spec sheet, but they show up as cracked mounts and rubbed-through cables.
One of the quiet killers is the tolerance on the hold-down lip. If that lip rolls inward by even 0.6 mm more than the design calls for, the battery case gets pressure in a spot it was never meant to carry. Over time, the plastic creeps and the strap loosens just enough to let the battery shift under hard braking. Buyers blame the strap, the battery, even the roads—but the real culprit is a tray dimension they never put a caliper on.
Then there’s the drain hole alignment. A hole drilled 2 mm off from the low spot turns a “drain” into a water trap, and every cold morning does the rest. The best trays don’t just meet a drawing; they hold those hidden tolerances tight enough that the tray disappears into the vehicle and does its job without anyone noticing. That’s the difference between a part you install once and a part you warranty twice.
Thermal Runaway Testing: From Smoke Tests to Certification
Early smoke tests are deliberately rough. A cell gets pushed past its electrical or thermal limits inside a sealed vessel while cameras and gas sensors watch for the first wisp of electrolyte vapor. The point isn’t to pass or fail—it’s to catch the moment venting starts, measure the gas mix, and figure out whether that specific chemistry tends to spit out hydrogen, carbon monoxide, or something nastier before flames even appear.
From there the work moves to calorimetry and propagation rigs. Accelerating rate calorimetry gives a heat release curve that shows how much energy the cell feeds back into its own failure, while module-level testing tracks how quickly thermal runaway jumps from one cell to its neighbors. Often the most useful output is the time gap between first vent and first flame, because that delay drives pack design, vent routing, and fire suppression choices.
Certification ties all of this into a structured chain. UL 9540A, UN 38.3, and IEC 62619 each cover different slices—transport safety, electrical abuse, fire propagation at the installation scale. Some fire marshals and permitting bodies only care about the final report, but an experienced reviewer will read backward through the whole dataset: smoke test gas yields, calorimetry heat rates, propagation intervals, and the full-scale burn. That continuity is what turns a stack of lab notes into a defensible safety case.
Lean Lines and Kanban Carts: Why Inventory Never Sits Still
On a lean line, kanban carts aren't a staging area—they're part of the production cadence. Each cart carries just enough parts for the next few cycles and rolls along a taped floor path to the workstation. When an operator pulls the first piece, the empty bin and its kanban card become the replenishment trigger: material is pulled into the flow, not pushed in. That leaves no room for inventory to sit idle; it's always in a state of being used.
The kanban system caps work-in-process by limiting how many carts can circulate. If a cart doesn't come back on schedule, the team knows there's a bottleneck or a quality issue upstream. This visual signal keeps inventory from quietly aging in a corner. Lines are often arranged in a tight U-shape or straight run, so the distance between stations is measured in seconds, not minutes, which further compresses any waiting time.
Unlike bulk pallets stacked in a warehouse, the containers on a kanban cart are small and standardized, easy for one person to move. That physical constraint encourages frequent, small-batch replenishment and makes the actual inventory count visible at a glance—you can see exactly how much is moving. In the end, stock becomes a pulse running through the shop floor rather than a static number on a ledger. As long as the line is running, the kanban carts never really stop.
Customer Specs to Packing Crates: The Final Inspection
Every crate leaves our floor only after matching the customer's spec sheet line by line. We don't rely on a quick glance or a supervisor's nod—each dimension, weight limit, and internal brace position gets checked against the original order. The final inspection isn't a formality; it's where mismatches get caught before they become a freight claim.
Our team walks the crate with the spec in hand, verifying foam density, corner reinforcement, and moisture barrier placement. If a tolerance is off by more than a few millimeters, the crate goes back for rework. No exceptions. This step has caught everything from a mislabeled forklift pocket to a missing humidity indicator card—details that would have meant downtime for the customer.
Once the inspection clears, the crate is sealed, tagged, and photographed from all six sides. Those photos and the signed checklist stay on file, tied to the job number. If a question ever comes up after delivery, we can show exactly what left the dock and how it matched the customer's specs at that moment.
FAQ
It starts with automated guided vehicles delivering pre-cut steel enclosures to the first station. Workers secure the internal racking, then robots apply thermal interface material before battery modules slide into place. By mid-morning, the line shifts to wiring harnesses and busbar torque checks, with each cabinet moving through a 14-step assembly sequence that changes based on the client's voltage requirements.
Every unit goes through a burn-in chamber at 45°C for 72 hours while cycling between 20% and 80% state of charge. The data logging system flags any cell imbalance above 2%, and those packs get pulled for rebalancing before final assembly. It's not just a pass/fail test; engineers review the charge curve to spot early signs of degradation.
Laser welding and adhesive dispensing are fully automated because micron-level consistency matters for thermal runaway containment. But final wiring inspection and torque auditing still rely on senior technicians who can feel when a connector isn't seated right. The factory deliberately keeps a hybrid line so complex custom orders don't get slowed by rigid robotics.
Outdoor units get a double-layer powder coat with salt spray resistance rated for 1,000 hours, plus a pressure-equalizing vent to handle temperature swings. Indoor cabinets skip the corrosion package but add acoustic dampening and narrower footprints. The assembly line switches between these variants using quick-change fixtures, so a run of 50 outdoor units can be followed by a single custom indoor prototype without major downtime.
Beyond the burn-in, each cabinet undergoes a dielectric withstand test at twice the rated voltage to check insulation integrity. Then it's placed on a vibration table that simulates transport over rough roads for 30 minutes. Finally, a helium leak test confirms the enclosure's IP54 or IP65 seal, depending on the specification.
The assembly area has a multi-zone detection system that monitors off-gas particles, not just smoke or heat. If a cell vents during testing, the cabinet is automatically moved to a segregated bunker with sand-based suppression. Workers also practice a quarterly drill where a thermal event is simulated, so the response time stays under 90 seconds.
The factory offers a glass-walled observation corridor above the main assembly hall. Customers can watch their specific cabinets being built, and there's a live dashboard showing test results for their batch. For companies with proprietary battery chemistry, a separate secure line blocks visual access but still provides real-time production data through a client portal.
Conclusion
Walking the production floor of a modern energy storage cabinet factory, the first thing that hits you is the rhythm: raw sheet metal enters one end and finished smart cabinets emerge from the other, but the real story lies in the middle. Robotic welding cells and fiber laser cutters run with a cadence that never pauses, trimming and joining enclosures to tolerances that would make a machinist grin. The battery tray is the quiet hero here—its flatness and hole positions are held within fractions of a millimeter, a spec most buyers never think about until a misaligned cell module ruins thermal contact. Those numbers aren't just for show; they determine whether a cabinet survives a short circuit or becomes a smoke plume.
Further down the line, thermal runaway testing turns theory into proof. Engineers deliberately push cells past their limits inside sealed chambers, watching smoke and temperature curves until the cabinet earns its certification. That same rigor carries into the logistics flow: lean lines with Kanban carts mean battery racks, busbars, and fasteners don't pile up in corners—they move only when the next station signals a need. By final inspection, every unit has been traced from customer spec to packing crate, with torque logs and test reports taped to the door. It's not flashy; it's the kind of factory discipline that separates a cabinet that merely looks solid from one that stays safe for ten years.
Contact Us
Contact Person: Manager Leng
Email: [email protected]
Tel/WhatsApp: 8613764878967
Website: https://www.unc-energy.com