Inflatable Seal Ball Segment Valve Solutions for Enhanced Flow Control
2026-08-16
What if your flow control system could handle abrasive media, pressure spikes, and imperfect sealing surfaces without constant maintenance? For many engineers, that’s not a hypothetical — it’s a daily headache. AVM’s inflatable seal ball segment valve solutions offer a fresh answer, combining robust shut-off with smooth modulation. Here’s a closer look at how they’re changing the game for enhanced flow control.
Leak-Tight Shutoff for Slurries and Sludges Without Packing Wear
Conventional valve packing rarely survives long in slurry or sludge service. The abrasive particles work their way between the stem and packing rings, grinding the seal material into fine debris and opening a direct path for leakage. Every stroke of the valve accelerates the damage, and soon the packing area becomes a constant drip point that maintenance crews must repeatedly tighten or replace. For thick, gritty media, this cycle is not just an inconvenience—it undermines process reliability and drives up operating costs.
A better approach eliminates the packing entirely. Pinch valves, for instance, use a replaceable elastomer sleeve that closes completely around trapped solids, creating a bubble-tight seal even when chunks of sludge are caught in the line. Knife gate valves with through-body design and no stem packing rely on a precision-machined gate and seat that shear through the media, while diaphragm valves isolate the working mechanism from the flow path altogether. In every case, the absence of a dynamic stem seal removes the main wear point and lets the valve achieve full shutoff without the constant need for adjustment.
Plants handling mining tailings, wastewater sludge, or chemical pastes see immediate benefits: fewer unplanned shutdowns, no fugitive emissions from stuffing boxes, and a valve that actually closes tight after thousands of cycles. The self-cleaning action of many packing-free designs also prevents solids from building up in the seat area, which keeps the shutoff reliable over time. For operators tired of chasing leaks, switching to a no-packing valve often proves to be the simplest long-term fix.
Segment Profiling That Matches Irregular Pipeline Flow Patterns
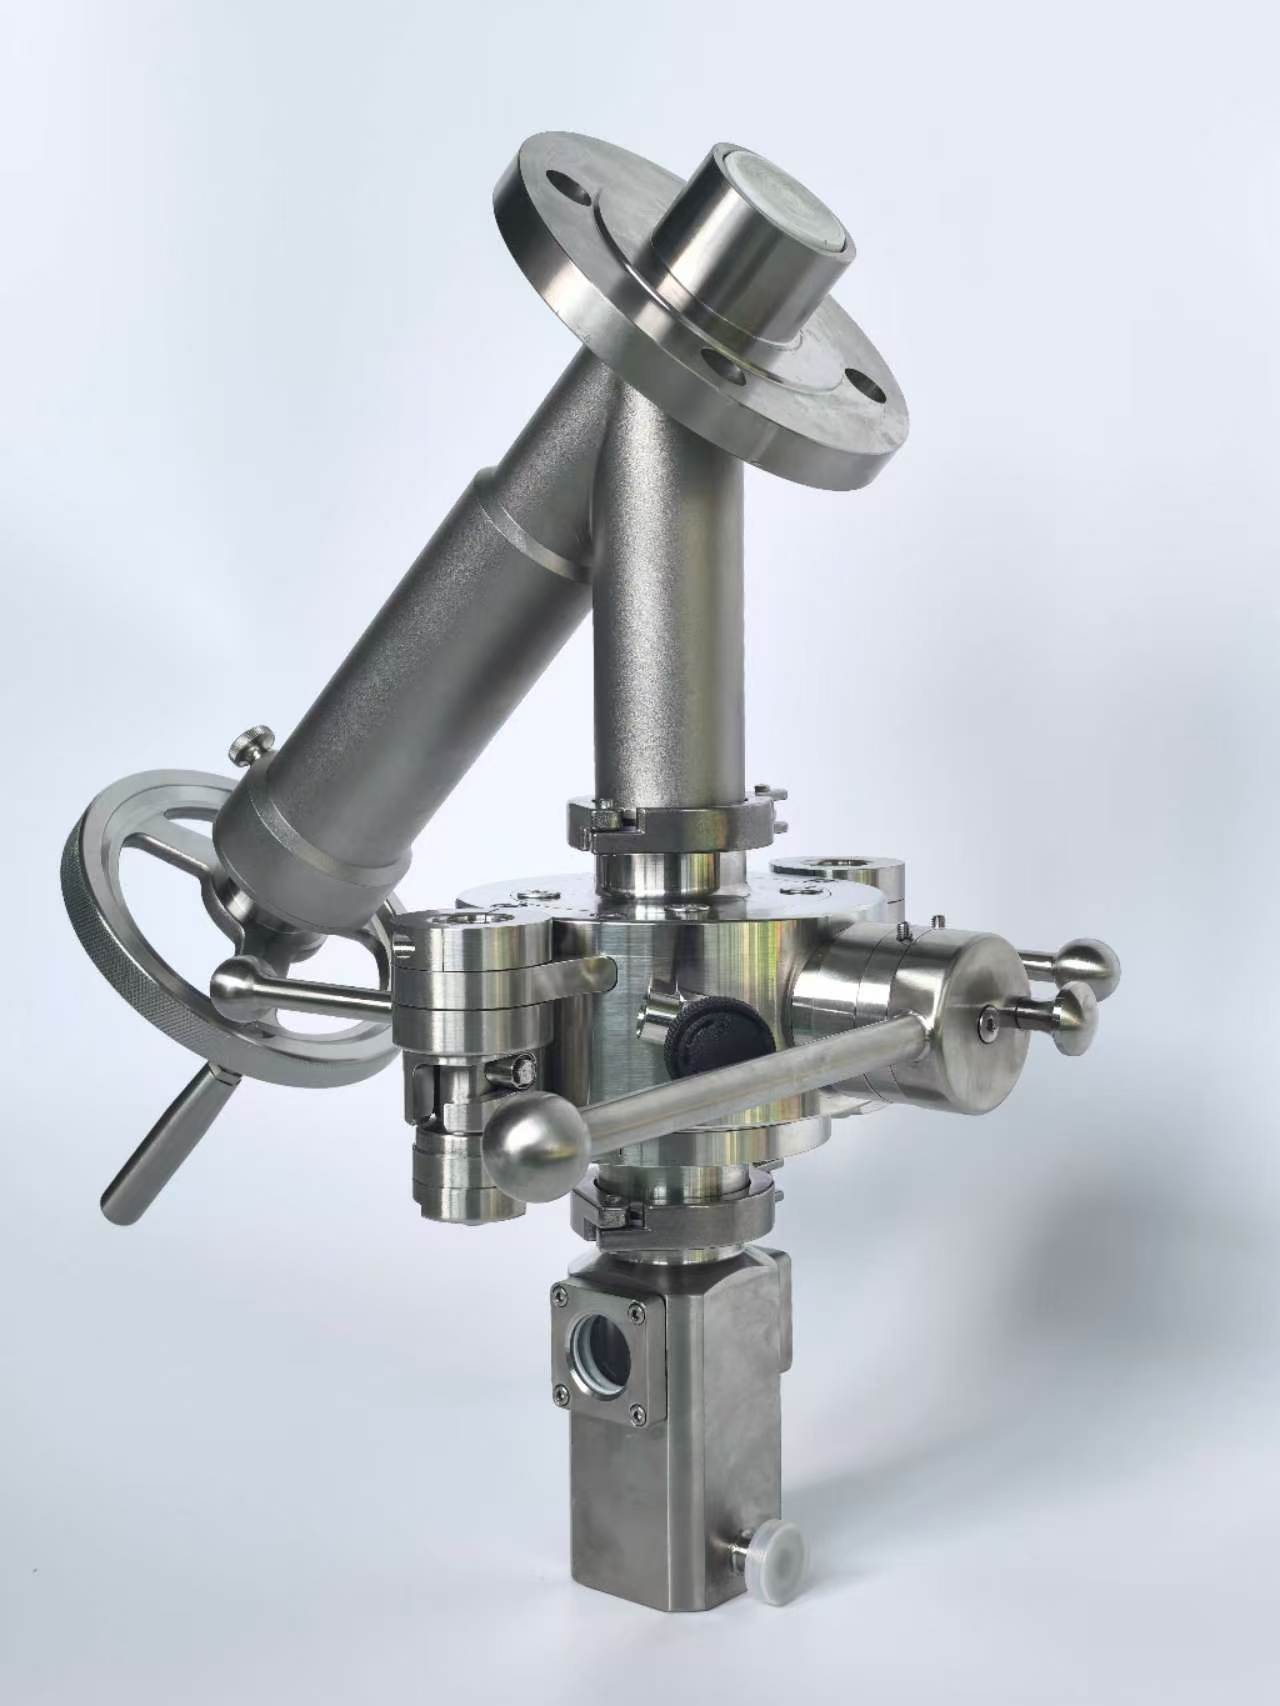
Irregular pipeline flow patterns often stem from slugging, terrain-induced liquid holdup, or rapid changes in throughput. Fixed-interval segmentation overlooks these local variations, leading to inaccurate predictions of pressure drop and erosion risk. A better approach treats the pipeline as a series of dynamically identified segments whose boundaries align with transitions in flow regime rather than arbitrary distance markers.
Field data from distributed acoustic sensing or high-frequency pressure transmitters can reveal where intermittent flow structures form and dissipate. By clustering these signals over time, operators can build a segment profile that shifts with actual operating conditions. For example, a segment might expand during steady production but split into smaller units when gas kicks or pigging operations push unstable slugs through the line.
The resulting profile feeds directly into integrity and efficiency models. Corrosion inhibitors can be targeted to segments with repeated slug impact, while compressor setpoints adjust to segments showing early signs of liquid accumulation. This segmentation method avoids the rigid assumptions of legacy tools and keeps the model aligned with what the pipeline actually experiences.
Controlling Cavitation Damage by Modulating the Seal Contact Zone
Cavitation erosion in mechanical seals often starts where the fluid film breaks down under rapid pressure fluctuations. By carefully reshaping the contact zone between the seal faces, you can shift the point of lowest pressure away from the solid boundaries. A slightly tapered or stepped land profile, for instance, encourages the formation of vapor cavities in the middle of the gap rather than at the edge, reducing the implosive energy that hammers the surface. This approach works best when the modulation is subtle enough to avoid reducing the load-carrying capacity of the film.
Another practical lever is to alter the surface texture within the seal contact zone. Micro-scale dimples or circumferential grooves can act as nucleation sites for stable cavitation bubbles, preventing sudden bubble collapse near the harder seal face. Because these features also influence the local pressure distribution, their geometry must be tuned to the specific operating conditions. A uniform pattern across the entire face rarely helps; instead, placing the texture only in the outer third of the contact area often yields a measurable drop in erosion without sacrificing sealing performance.
Field experience shows that even small changes in the contact zone's boundary shape can redistribute the cavitation damage pattern. By moving the high-velocity jet impact point away from the softer carbon face and toward a hardened insert or a sacrificial ring, the seal's service life can be extended significantly. The key is to treat the seal contact zone not as a fixed geometric constraint, but as a design variable that can be modulated to steer cavitation energy where it causes the least harm.
Isolation Reliability Where Conventional Ball Valves Struggle
Conventional ball valves usually rely on soft seats—PTFE, reinforced nylon, or similar polymers—to seal against the ball. In clean, moderate-temperature service that works well enough. But once solids, scale, or pipe debris get into the line, those seats become the weak point. Particles embed in the soft material or scratch the ball surface, and each cycle shaves away a little more sealing area. A valve that closes fully in the handwheel can still pass a surprising amount of fluid past the seat because the sealing path is no longer continuous.
Thermal swings make things worse. The ball, body, and seat expand and contract at different rates, opening micro-gaps at the seat interface exactly when isolation matters most. High differential pressure during closing can also drive fines into the seat pocket, preventing the ball from rotating the final few degrees. Operators then force the handle or actuator harder, which deforms the seat further and creates a permanent leak path instead of a tight shutoff.
What often gets overlooked is erosion on the leading edge of the ball. After thousands of cycles, especially with flashing liquids or abrasive slurries, that edge rounds off and no longer wipes the seat clean. Maintenance teams discover the problem during line break or lockout, when the valve is already supposed to be isolated. Achieving dependable isolation in these conditions means moving beyond a basic soft-seat ball valve—either to seats that self-compensate for wear, to hard-faced trim, or to a design that isolates the seats from the full brunt of the flow when the valve opens and closes.
Jam-Free Operation in Sticky or Particulate-Laden Media
Handling sticky slurries or fluids loaded with fine particulates quickly exposes the weaknesses of conventional flow paths. Small clearances, sharp corners, and dead zones invite material to accumulate, harden, or bridge, turning a simple transfer into a recurring cleaning chore. The real problem isn't just viscosity—it's the way the medium interacts with any surface that gives it a place to cling or settle.
A jam-free design starts by removing those traps. Internal geometries open up to let solids pass without shearing or compacting, while moving parts either avoid direct contact with the process fluid or use a continuous wiping action. Surface finishes matter too: a polished, non-porous contact face reduces adhesion, and the absence of narrow seal gaps prevents particles from wedging into places that later seize up.
The result is a device that keeps cycling even when the feed consistency swings or the solids concentration spikes. Operators can run longer batches without slowing down to clear blockages, and the need for bypass lines or frequent teardowns drops sharply. In wastewater, food processing, or adhesive manufacturing, that translates to a line that doesn't fight the product it's moving.
High-Performance Materials for Acidic, Caustic, and Hot Streams
Industrial fluid handling rarely offers clean water at room temperature. Many processes push aggressive chemicals through pipes and valves at elevated temperatures, where ordinary alloys soften, corrode, or crack within months. For acidic, caustic, and hot streams, material selection shifts from simple compatibility charts to a careful balance of corrosion resistance, thermal stability, and long-term mechanical strength. Engineers often look beyond standard stainless steels to high-nickel alloys, titanium grades, fluoropolymer linings, and engineered ceramics, each chosen for how it behaves under a specific combination of acid concentration, pH, temperature, and flow velocity.
Acidic streams, whether sulfuric, hydrochloric, or organic acids, attack metals through general thinning or localized pitting. High-performance materials such as Hastelloy C-276 and titanium grade 7 resist these mechanisms by forming stable passive films that remain intact even in reducing or oxidizing environments. Caustic streams, by contrast, present a different failure mode: caustic stress corrosion cracking. Nickel and nickel-copper alloys like Monel 400 and Inconel 600 are preferred here because they maintain ductility and resist cracking in hot sodium hydroxide solutions where stainless steels would fail quickly. For both acidic and caustic conditions above 150°C, fluoropolymers like PTFE and PFA offer nearly universal chemical resistance, though their maximum service temperature and mechanical strength limit them to lined or non-structural components.
Hot streams add another layer of difficulty. Even when a material resists chemical attack at ambient temperature, elevated heat accelerates corrosion kinetics and can trigger creep, thermal fatigue, or phase precipitation that embrittles the alloy. Duplex stainless steels, with their mixed austenite-ferrite microstructure, perform well in hot chloride-bearing environments up to about 300°C, while superalloys like Inconel 625 retain strength and oxidation resistance above 600°C. For the most demanding acidic, caustic, and hot combinations, no single metallic material is ideal; instead, designers use ceramic-lined piping, silicon carbide heat exchangers, or glass-lined reactors to isolate the process fluid entirely. The key is not chasing a universal super-material, but matching each zone of the system to the specific chemistry and temperature it will actually see.
FAQ
It's a valve design that combines a segmented ball with an inflatable sealing element. When the valve needs to close, the seal inflates to press tightly against the ball segment, eliminating leakage and giving precise throttling control even with slurries or viscous fluids.
Mining, wastewater treatment, chemical processing, and pulp and paper operations see the biggest gains. Anywhere that handles abrasive slurries, scaling liquids, or media prone to clogging conventional valves.
Compressed air or hydraulic fluid inflates an elastomer seal around the ball segment. The seal expands to hug the segment's surface, creating a bubble-tight shutoff. When opening, the seal deflates first, so there is minimal friction and no scraping damage.
The deflate-before-rotate sequence means the sealing surface isn't dragging across the ball under pressure. That reduces wear, prevents jamming from solids buildup, and extends service life in applications where standard valves fail quickly.
Yes, within specified elastomer limits. For extreme temperatures or aggressive chemicals, specialized seal materials like Viton, EPDM, or silicone are selected. Pressure ratings depend on body design, but many models handle up to 10 bar and above.
Regular inspection of the inflatable seal for cracks or swelling is essential. Keep the inflation air supply clean and dry. Lubricate the stem bearings occasionally, and replace the seal at the first sign of uneven wear to avoid unexpected downtime.
If you need precise, repeatable flow modulation rather than just on/off service, the segmented design is superior. The inflatable seal adds tight shutoff and protection from abrasive media, making it ideal for throttling slurries where standard full-bore valves erode quickly.
The inflatable seal is the primary wear item. Premature failure usually comes from over-pressurizing the inflation line or using incompatible media. Staying within the recommended inflation pressure and verifying chemical compatibility with the seal material prevent most issues.
Conclusion
Conventional ball valves tend to struggle once slurries, sludges, or sticky particulates enter the picture—packing wears out, seats erode, and isolation becomes unreliable. The inflatable seal ball segment valve takes a different route. Instead of relying on a fixed packing set, the seal inflates to create a leak-tight shutoff that handles solids-laden flows without the usual wear points. Segment profiling is shaped around the actual pipeline flow pattern, so the valve works with irregular velocity profiles rather than forcing a generic spherical bore. During closure and throttling, the seal contact zone is modulated to keep cavitation damage in check, which matters a lot in high-energy liquid services where standard ball valves pit and fail early.
The same design also prevents jamming in media that would normally clog or bind a rotating ball. Because the segment does not have to sweep across a full-body seat, sticky and particulate-laden streams pass through with less torque and fewer hang-ups. Material selection extends the operating window to acidic, caustic, and high-temperature streams, so the valve stays functional where chemical attack or thermal cycling would degrade ordinary elastomers and metals. Taken together, these features give operators a more predictable isolation and flow-control point in applications that routinely punish conventional ball valves—from mining slurries and wastewater sludge to aggressive chemical transfer lines.
Contact Us
Contact Person: Ananda
Email: [email protected]
Tel/WhatsApp: 8619016718200
Website: https://www.wzaomi.com