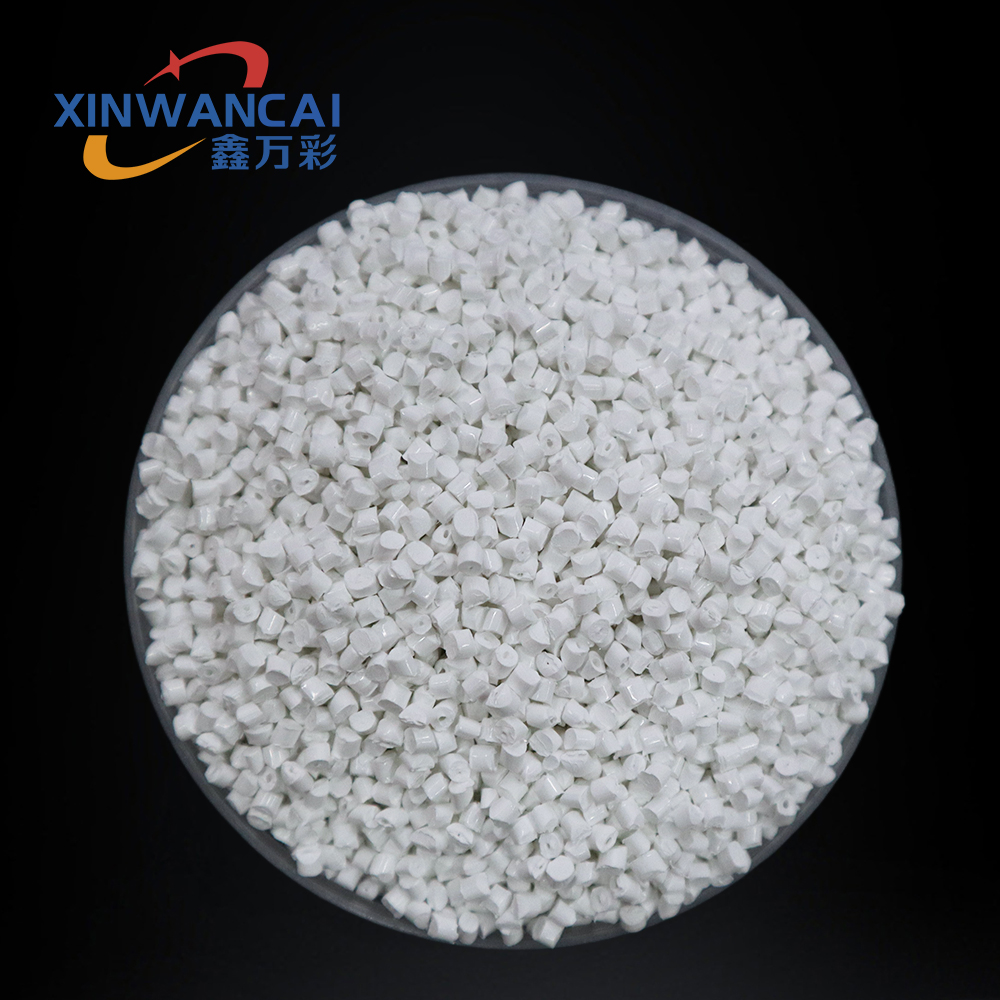
White Masterbatch Original Manufacturer Guide to Superior Color Consistency
2026-10-08
White masterbatch is one of those materials nobody notices until it fails. A slight yellow tint, uneven opacity, or poor dispersion can turn a premium product into a rejected batch. Most brands chase consistency by testing more samples, but the real answer lies further back—in the hands of the original manufacturer. Xinwancai cuts out the usual guessing game by controlling raw materials, processing, and quality checks from start to finish. This guide reveals how that direct control translates into superior color consistency, and what to look for when choosing a white masterbatch partner.
What Actually Causes White Masterbatch to Shift from Bright to Bone
The drift from bright white to bone often starts with the titanium dioxide itself. Rutile grades with heavy organic coatings or trace iron levels can push the undertone away from a clean blue-white toward a warmer, yellowish cast. When a processor switches to a lower-cost anatase or a blended pigment, that shift can show up almost immediately in the molded part, even before any thermal history is added. Phenolic antioxidants in the carrier resin can also react with TiO2 under heat, forming yellow-brown complexes that accumulate over multiple heat cycles and get mistaken for simple resin yellowing.
Processing conditions play a bigger role than most people want to believe. Running the masterbatch at barrel temperatures above the resin's recommended range, or letting residence time stretch too long, degrades the polymer and releases aldehydes and ketones that dull the white. Moisture in the resin or pigment can make the problem worse by promoting hydrolysis, so the bone hue may not show up until a few days after molding. Even the letdown ratio matters: too little masterbatch forces higher melt temperatures to get the same opacity, which circles right back to the same degradation pathway.
The Base Resin Property That Predicts Long-Term Shade Stability
Long-term shade stability in resin-based restoratives rarely hinges on the pigments alone. The base resin's water sorption behavior is a far more reliable early indicator of how well a material will hold its color over years of service. Resins that pull in even small amounts of moisture tend to swell slightly at the matrix-filler interface, opening microscopic pathways for extrinsic stains from coffee, tea, and tobacco. More importantly, that absorbed water gradually hydrolyzes silane coupling agents and ester linkages within the methacrylate network, creating a rougher, more porous surface that scatters light differently and makes the restoration look dull or chalky long before any actual color change is measurable.
A resin with inherently low water uptake, by contrast, keeps its filler particles tightly bound and its surface densely cross-linked. This limits the depth to which staining molecules can penetrate and slows the breakdown of the resin-filler bond. In clinical terms, that means the restoration maintains its original translucency and gloss longer, and any superficial discoloration remains easy to polish away because it has not become embedded in a degraded matrix.
So when evaluating shade stability claims, look past the pigment package and ask about the base resin's equilibrium water sorption value. A low-sorption monomer system is not a guarantee of perfect color retention, but it is the single most predictive resin property available—and one that separates materials intended for long-term anterior use from those that will begin to look flat and stained within a few years.
Titanium Dioxide Dispersion Without Breaking the Pigment Matrix
Dispersing titanium dioxide in a liquid vehicle often involves a trade-off. Apply too little mechanical force and the dry pigment agglomerates remain intact, leading to poor color development and surface roughness. Apply too much shear, however, and you risk fracturing the pigment matrix itself—the very crystalline structure and surface treatment that give TiO2 its opacity, durability, and weather resistance. The goal is to separate agglomerates at their contact points without grinding down the primary particles or cracking their inorganic coatings.
One practical route is to combine a compatible wetting agent with staged, low-to-moderate shear mixing. The dispersant first displaces air and moisture from the pigment surface, lowering interfacial tension so the vehicle can penetrate between particles. Then a short high-shear step breaks loose agglomerates, followed by gentler mixing to stabilize the dispersion. Particle size monitoring is essential here; once the curve shifts from agglomerate breakdown to primary particle fracture, the process has gone too far. Keeping the TiO2 matrix intact preserves not only optical performance but also long-term film integrity under UV exposure and humidity cycling.
How Screw Speed and Barrel Profile Quietly Rewrite Your Color Target
Screw speed often gets blamed for shear heating, but its effect on color goes deeper. Faster rotation can break up pigment agglomerates, yet excessive speed lowers residence time distribution and leaves some masterbatch poorly dispersed, causing washed-out or streaky tones. Even with identical colorant loading, a 20% change in RPM can shift L* or a* enough to fail a visual match.
Barrel profile compounds the issue. A flat profile versus a reverse or barrier section changes how melt temperature develops along the screw. If the compression zone is too short or too aggressive, local viscosity drops before pigments fully wet out. That means the same blue concentrate might read more violet under one profile and greener under another, simply because the carrier resin and pigment didn't see the same thermal history.
Together, screw speed and barrel temperature zones quietly move your color target away from the lab plaque. Operators who chase the colorimeter by adding more pigment often miss that the real variable is mechanical. Mapping color shift against RPM and barrel set points for each formulation stops the silent drift.
Reading a Spectrophotometer Curve Like a Plant Manager Instead of a Lab Tech
A lab tech hunches over the printout, cross-checking absorbance values against a reference table, muttering about a 0.002 deviation at 450 nm. A plant manager glances at the same curve and sees something else entirely: did the batch drift off-spec somewhere in the middle, or is this just normal noise? The manager isn't paid to admire the instrument's precision; they're paid to keep the line moving and the waste bin empty. So instead of zooming into individual data points, they scan the curve's overall posture—where it starts, how steeply it rises, whether it plateaus or collapses—and ask the only question that matters: does this look like yesterday's good run, or does it look like the batch we had to scrap last month?
That practical eye changes what gets flagged. A technician might report every tiny shoulder or baseline wobble as an anomaly worth investigating. A manager learns to ignore the harmless fingerprints of a cuvette that sat a few seconds too long and instead watch for the red flags that correlate with real production problems: a curve that should peak sharp but comes out round, a repeated dip at the same wavelength across multiple samples, or a baseline that creeps upward in a way that screams contaminated solvent. These patterns aren't in any manual—they come from living with the process day after day until the curve becomes a kind of signature, and a wrong signature sets off alarms before the quality lab even finishes its report.
Eventually the manager connects the curve's shape to what was happening on the floor at the moment the sample was pulled. A high-temperature spike during the reaction shows up as a flattened peak; a rushed rinse step leaves a telltale hump around 600 nm. That's the real skill—not reading the spectrophotometer, but reading the story it tells about pumps, valves, and human error. Lab techs produce the data. Plant managers use it like a rearview mirror, not to admire the scenery but to keep the next batch from driving off the same cliff.
When a New TiO2 Supplier Forces a Full Re-Qualification
Switching to a new TiO2 supplier rarely starts with a simple purchase order. In coatings, plastics, and inks, titanium dioxide is not a drop-in commodity. Every grade carries its own particle size distribution, surface treatment, and oil absorption profile. If incoming material differs enough from the incumbent, the downstream formulation can shift in gloss, dispersion time, and weather resistance. That triggers a full re-qualification, not because the new supplier is necessarily worse, but because the product was built around the previous material's quirks.
The re-qualification effort often begins with a lab-scale comparison. Teams run drawdowns, measure tint strength, and check for aggregate formation under a grind gauge. They also age samples in accelerated weathering cabinets, since TiO2's photocatalytic activity can vary with the exact alumina or silica coating. A few weeks of testing can turn into months if color drift appears in a tinted base or if dispersion energy needs to be adjusted on a production line. Every test adds cost, but skipping steps is how a quiet formula change becomes a field failure.
What makes the situation difficult is that the new supplier may promise equivalent performance on paper. Certificates of analysis rarely capture the subtle interactions between TiO2 and dispersants, resins, or other pigments. A full re-qualification is really about rebuilding confidence in the entire system. Until that confidence exists, the old material stays on the line, even at a higher price or with longer lead times.
FAQ
Original manufacturers control the full production chain—formulation, raw material intake, compounding. Traders often source from multiple tollers, which adds variability. Direct control means we can tweak dispersion or pigment ratio on the spot to keep the white shade locked.
We keep a master reference standard for each product and measure every batch against it with a spectrophotometer. Raw materials get pre-qualified by lot, and production logs track screw speed, temperature, and residence time. Anything outside our internal tolerance is reworked, not shipped.
Titanium dioxide carries most of the hiding power and base tone. If particle size, surface treatment, or purity shifts, the white moves from warm to cool. We stick to one approved TiO2 grade per formulation and check incoming material for tinting strength before it goes into production.
Poor dispersion leaves agglomerates that scatter light unevenly, making the part look dull or grayish. Good dispersion gives uniform opacity and a clean, bright white even at lower addition rates. We monitor it with pressure-rise tests and film analysis, not just a visual check.
Shade can shift because the carrier resin changes refractive index and how the pigment wets out. We develop separate formulations for each polymer and adjust pigment loading or additives to compensate. Customers get a shade card per resin system so they can confirm the match before full-scale use.
Each lot goes through melt flow index, filter pressure value, and color measurement against the reference standard. We also extrude or mold sample plaques and measure L*a*b* values under D65 lighting. Only lots that pass both physical and optical checks get released.
Keep the material sealed and dry, away from direct sunlight and big temperature swings. Moisture pickup can cause hydrolysis in some carriers and create specks. Use consistent let-down ratios and mixing times, and avoid blending masterbatch from different lots in the same hopper without checking homogeneity first.
For demanding applications we typically hold a Delta E below 0.5 against the approved standard. General-purpose grades usually run under 1.0. Those numbers are tighter than many industry norms because visual consistency in final parts cuts downstream rejects significantly.
Conclusion
Achieving reliable white masterbatch color consistency starts well before the extruder reaches steady state. The familiar drift from bright white to bone is rarely a single failure; it comes from small shifts in raw material and process that compound over time. The base resin's molecular weight distribution and melt flow characteristics quietly set the ceiling for how evenly titanium dioxide can be distributed without crushing the pigment particles. When dispersion energy is too high, the TiO2 matrix fractures, lowering hiding power and shifting the visual tone. Screw speed and barrel temperature profile are no less influential—each zone either preserves or erases the dispersion work done upstream. A plant that treats these as fixed setpoints rather than variables to be monitored will keep chasing shade adjustments that never hold.
Reading a spectrophotometer curve the way a plant manager does means looking past the single L* value and asking where the curve tilts in the yellow-blue axis. A slight shoulder in the 500–560 nm range often signals residual resin degradation or an incompatible additive package, not a pigment problem. This kind of practical reading helps separate real batch drift from instrument noise. When a new TiO2 supplier enters the picture, the change is never a drop-in replacement. Surface treatment, particle size distribution, and trace metal content all interact with your specific screw configuration and barrel conditions. That forces a full re-qualification: start with small-scale trials, map the response across your normal screw speed range, and compare not just color but also rheology and filter pressure. Only then can you lock in a new raw material without risking the color target your customers see on the line.
Contact Us
Contact Person: JACK
Email: [email protected]
Tel/WhatsApp: 86 18650130917
Website: https://www.xinwancai.com/